Skip to content

What a 230 V supply will actually run

Most workshop machines are limited by the building rather than by the machine. A 230 V, 16 A socket sets a ceiling on what any welder or plasma cutter can draw continuously, and that ceiling is usually reached long before the machine’s rated maximum.

Most workshop machines are limited by the building rather than by the machine. A 230 V, 16 A socket sets a ceiling on what any welder or plasma cutter can draw continuously, and that ceiling is usually reached long before the machine’s rated maximum.

Which welder suits your metal?

You have an ordinary workshop socket
Duty cycle will decide everything. A powerful machine is not ruled out; it will simply be limited in how long it runs.
Your breaker only trips at start-up
That is a trip-curve and inrush problem, not a shortage of power.
You feed the machine through an extension lead
Cross-section and length matter as much as the socket: voltage drop is paid for in performance and in heat.
You are considering heavier equipment
The question is no longer the machine but the installation: a dedicated circuit, and possibly three-phase.

Picking by the metal

Intermittent welding

Most workshops: a few beads with pauses between them. The duty cycle is almost never reached.

Prolonged grinding

A grinder draws less than a welder but draws it continuously. That is a different regime, and harder on an undersized cable.

Compressor and plasma together

The compressor restarts during the cut: it is the two inrush currents adding up that trips the circuit, not either on its own.

Direct-on-line machines

Bench grinder, bandsaw, pillar drill: starting current far exceeds rated current, briefly.

What matters at the arc

Duty cycle, again
It says how long out of ten minutes the machine can hold a given current. On a domestic supply that is the practical limit, well before the quoted power.
The breaker curve
A C curve tolerates a bigger, longer inrush than a B curve. It is often the only difference between a machine that starts and the same one tripping the circuit.
Cable cross-section and length
An extension lead too thin or too long drops the voltage: the machine loses bite and the cable warms. A lead left coiled on its drum warms more still.
Current drawn, not power quoted
It is the maximum current on the rating plate that compares to the breaker rating. Power in kilovolt-amperes compares directly to nothing.

Which figure for which metal

SymptomMost likely causeWhat to look at
The breaker trips at start-upInrush current and trip curveThe breaker’s curve, not its rating
The breaker trips after several minutesRunning beyond the duty cycleDuty cycle at the current in use
The machine lacks biteVoltage drop in the supplyExtension lead cross-section and length
The socket or cable gets warmPoor contact or undersized cableThe state of the socket and the cable rating

Where it goes wrong at the bench

Fitting a bigger breaker
The breaker protects the cable, not the machine. Raising its rating without changing the cable removes the protection instead of solving the problem.
Using a coiled extension lead
A lead left on its drum forms a coil that heats. Unwind it completely, even if it means a heap on the floor.
Reading the power and not the current
Two machines with the same quoted power can draw very different currents depending on power factor. It is the current that decides.
Stacking adapters
Every extra contact is a resistance and a hot spot. At welding currents you can feel it by hand.

By the welder you are

The garage workshop
A dedicated circuit with generous cross-section beats a bigger machine on a shared socket.
A station in an outbuilding
Cable length becomes the dominant factor: voltage drop is worked out before buying, not after.
Regular professional use
Three-phase, where it is available, changes the picture: a higher duty cycle at the same current, and less strain on the circuits.

Consumables, duty cycle and working life

A workshop supply needs little maintenance, but it does give warning. A blackened socket, a warm cable, a smell of heat after a long job: those signals always come before the failure.

  • Check the state of the sockets and plugs used for heavy loads.
  • Unwind extension leads fully, and prefer one lead to two joined end to end.
  • Check the terminal tightness of a dedicated socket after a few months of use.
  • Have the installation checked by an electrician before adding heavy equipment, rather than after.

Safety

The risk of an undersized supply is not the outage: it is a cable heating inside a conduit or a wall.

  • Never defeat or bypass a protective device.
  • An RCD upstream of the working area, as well as the breaker.
  • Unplug before working on a machine, including to change a disc.
  • Any consumer-unit work belongs to an electrician: it is the one point on this page where the advice is not to do it yourself.

What we chose, and on what basis

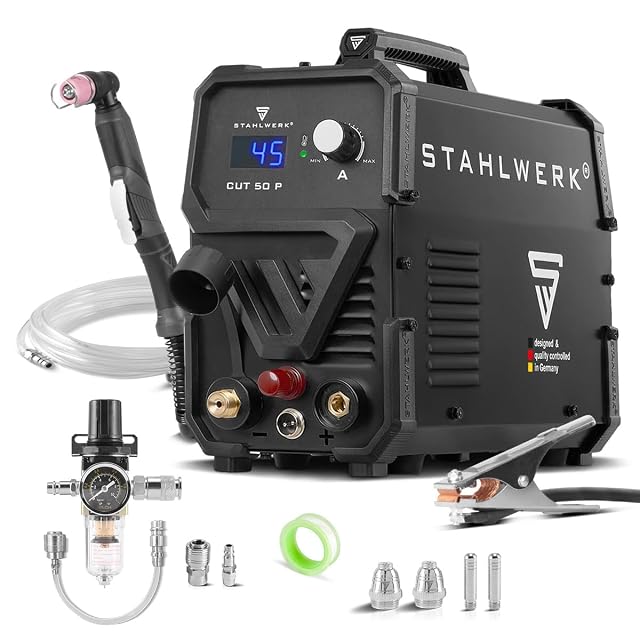
  1. STAHLWERK CUT 50 P

    15–45 A · 15 mm (0.59 in) steel / 8 mm (0.31 in) stainless / 5 mm (0.20 in) aluminum · €330

    The first machine here that publishes its cut thickness for three materials instead of one — which is the whole specification.

    Best for: A workshop cutting steel plate and section up to about 10 mm (0.39 in), cleanly

    8.1/10

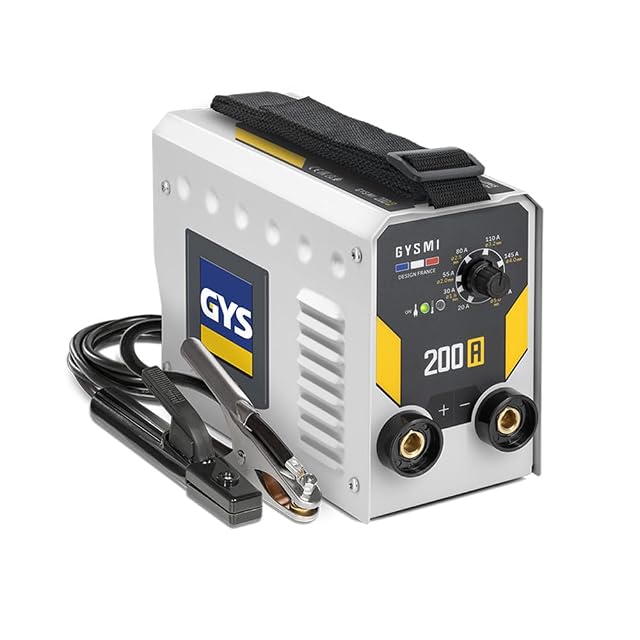
  2. GYS GYSMI 200 A

    200 A · 230 V · rutile, basic, stainless, cast iron to Ø 4 mm (0.16 in) · €263

    The only machine in this batch live on all six markets, and the only one that names the electrode types it is built for.

    Best for: Someone who welds cast iron or runs basic electrodes and wants the machine to cope

    8.1/10

    ≈ $405

The questions welders ask

Why does my machine trip the breaker?

Usually because the demand exceeds what the circuit can hold, or because the breaker curve is wrong for an inrush load. Welding inverters draw a surge at strike, and a curve intended for lighting reacts to that. Which curve is standard varies by country — in Britain a type B is common on domestic circuits, in Spain a type C — so the right answer depends on where you are.

Do I need three-phase?

Only for the heaviest equipment. On this site, one plasma cutter requires 400 V three-phase and everything else runs on 230 V single-phase. If you have three-phase available, it spreads the load and machines behave better under sustained use; if you do not, it is a substantial installation rather than an upgrade.

What size extension lead should I use?

It depends on current and length: the longer the run, the bigger the cross-section. A heavy site lead costs little next to a machine held back, and it lasts for years.

Can I plug a welder into a kitchen socket?

Electrically, often yes at low settings; in practice the circuit is shared and protected for another purpose. A dedicated circuit avoids tripping the rest of the house on every bead.

Would a voltage stabiliser help?

Not for this kind of load: such devices are not sized for a welder’s inrush. The remedy is cable cross-section and circuit rating, not a box in between.

Will a generator do?

Provided it is generously sized and delivers a clean waveform: the electronics in welding inverters are sensitive to it. The power needed is far above the average power consumed.

How do I know a cable is getting too hot?

By hand, after a long job: a warm cable is normal, a hot one is not. A blackened or deformed socket is a later and more serious signal.

Is three-phase always better?

Where it is already available, it allows a higher duty cycle and puts less strain on the installation. Having it installed for occasional use rarely adds up: the connection cost far exceeds the difference in performance.

Each welder, and the metal it is meant for

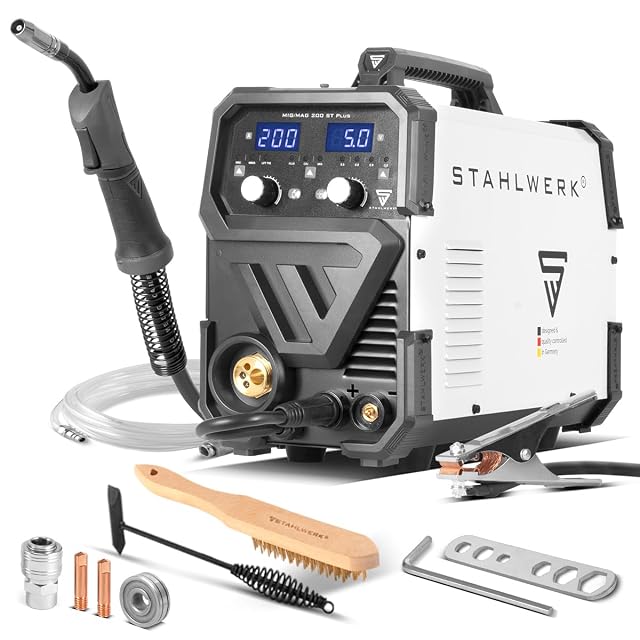
STAHLWERK MIG/MAG 200 ST

For work that: A first serious MIG that will still be adequate after two years of use
Where it is best: Synergic control: you set the material and thickness, the machine sets the wire speed

Where it is worst: The duty cycle is not stated with its temperature in the listing, so 200 A is a ceiling, not a working figure

Read the full review →

STAHLWERK CUT 50 P

For work that: A workshop cutting steel plate and section up to about 10 mm (0.39 in), cleanly

Where it is best: Three cut thicknesses published, by material — the only honest way to quote a plasma cutter

Where it is worst: 45 A maximum, so 15 mm (0.59 in) is the real ceiling in steel

Read the full review →

GYSMI 200 A · $405

For work that: Someone who welds cast iron or runs basic electrodes and wants the machine to cope

Where it is best: Names the electrode families it handles — including basic and cast iron, which cheaper machines avoid mentioning

Where it is worst: €263, against €90 to €140 for the machines above it

Read the full review →

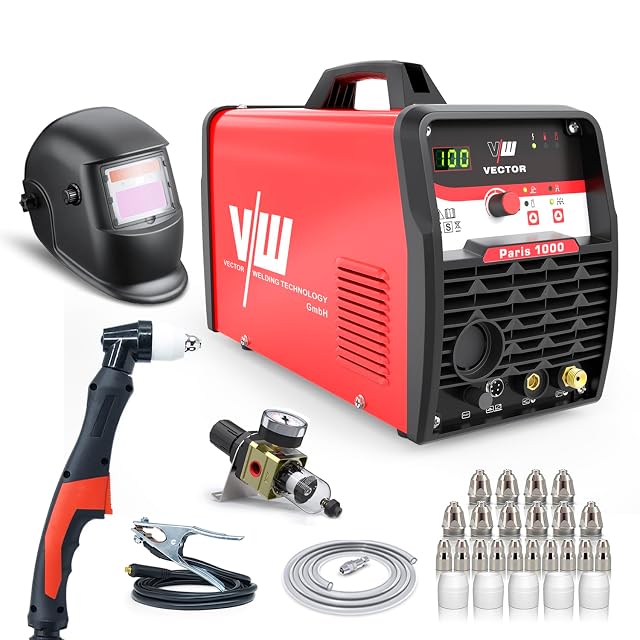
VECTOR WELDING Paris 1000 (100 A, 400 V)

For work that: A workshop with a three-phase supply and plate that defeats everything else

Where it is best: Forty-five millimeters of severance — nothing else here is close

Where it is worst: 400 V three phase: most domestic and many small workshops cannot power it

Read the full review →

What it will consume

Tips, nozzles, wire and gas from the same aisle, at the price we read. Confirm they suit the machine you choose before ordering: it turns on the torch and the part number, which the product page gives.

The call, in one line

Comparisons that are worth reading

Welder against welder, where the comparison is already written up.

What this selection rests on

The welders here are taken from the catalog of this site. Specifications come from the maker and from the Amazon product page; prices are what Keepa reported for the date shown, and both move. The order rests on declared specifications, on stated strengths against stated limits, and on price. No machine here has struck an arc in our hands, and nothing on this page pretends it has.

Last checked on

Prices quoted in these summaries are dated readings. The live price is shown next to each product.

The tool we use ourselves

Chosen your machine? Now buy it at the right price.

Welders and plasma cutters swing by a hundred dollars or more across the year, and the biggest "discounts" often land at prices the same model sold for six weeks earlier. UniverTrack tracks the real price history across retailers, spots fake reductions, and alerts you when it is genuinely the moment to buy.

Real price historyBuy-now alertsAI buying assistant
Try free for 14 days →
No commitment · Cancel in one click · 5 languages